Why Electronics Manufacturing Delays Build Up Before Production Starts
- james-sweetlove
- 875 reads
For prototype and NPI builds, material tracking, late design changes and delayed supplier input can consume days before the production line starts.
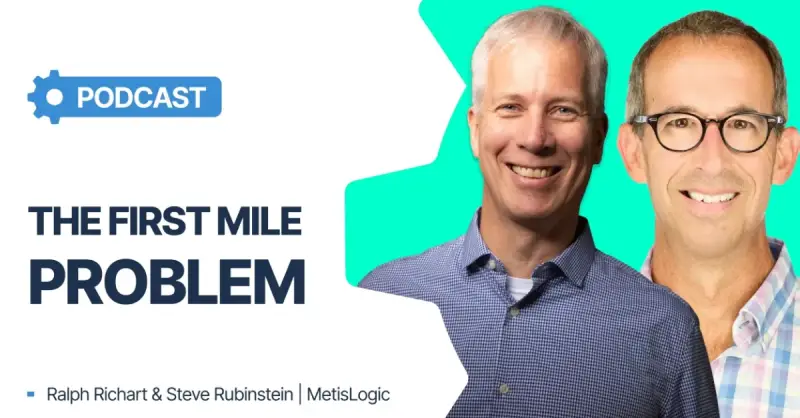
For a prototype or new product introduction (NPI) build, the production line may be ready long before the job is. The interval between completing a design and starting manufacturing can absorb days in procurement, part changes, coordination and readiness checks. MetisLogic calls this interval the “first mile” of manufacturing. The company’s founder, Ralph Richart, and chief operating officer, Steve Rubinstein, describe it as a messy middle where teams must turn a design and a quote into a confirmed plan for a physical build.
That distinction matters most when production runs are small, product mixes are high and each build has little schedule slack. A few days spent establishing whether parts have arrived, whether they are allocated and whether the design is still current can consume a large share of a short build schedule. Buying faster equipment or automating warehouse storage may improve other parts of a factory, but those measures won’t resolve an unnoticed component change or an incomplete material record.
The gap between design and a buildable job
The first mile begins after design work is considered complete and ends when manufacturing starts. It includes procurement, program management, design for manufacturability and assembly (DFM/DFA), and the handoff to production. A contract manufacturer may already have quoted the work, but a quote alone doesn’t establish that the ordered parts, current design and factory plan are aligned.
Richart and Rubinstein identify material workflow as the missing connective tissue. Teams need to know what has been ordered, what has arrived, what remains outstanding and whether the available material matches the job that production is expected to build. Those questions can span procurement, receiving, program management and production planning. If each group keeps its own partial view, a project can appear ready in one system or conversation while important parts are still missing or their status is unclear.
The resulting delay is easy to misread. A late shipment from a factory may appear to call for more machine capacity, extra automation or a faster production process. But if requirements changed and the change wasn’t caught before work reached the floor, machine speed doesn’t address the cause. The design, material and build instructions still need to be brought back into agreement.
Warehouse automation has a similar limit. Richart and Rubinstein say systems designed around large component reels may not reliably interpret labels on bags of cut tape. An automated rack or receiving station can help with the handling it was designed for, but it won’t necessarily answer whether a particular small-lot component has arrived, been identified and been assigned to the correct build. For manufacturers with many part types and relatively small quantities, the material record itself is part of the production problem.
Why small builds feel the delay more sharply
High-volume, repeat production has characteristics that can make first-mile delays less visible. A stable bill of materials (BOM), bulk purchasing and recurring orders help teams establish a familiar flow. When a build runs for eight weeks, spending a week or two getting materials and information to the shop floor takes up a smaller share of the total schedule than it does on a ten-piece job expected to finish in a week or two.
That comparison changes the priorities. On a short NPI or pre-production build, four or five days in the first mile can put the schedule under immediate pressure. Even if the production process itself is efficient, there may be too little time left to absorb a procurement problem, a design adjustment or uncertainty about whether a kit is complete. Compressing the interval before production can therefore improve the delivery timeline without changing machine cycle time.
In established production, teams may have bought components well in advance or arranged scheduled deliveries. Early builds often have less protection. The project may depend on current availability, with a part that seemed obtainable yesterday no longer ready when the build needs it. Richart says program managers often carry much of the work of reconciling those changes while also trying to deliver the right materials and information to production.
Richart connects the increased attention to the first mile with supply conditions that remained unsettled after the COVID disruption. He describes a difference between sustaining production, where a manufacturer may have planned inventory and scheduled supply, and NPI work, where teams can be operating close to what is available at the moment. In that setting, the build plan must respond as parts, timing and requirements change. A production team can’t rely on the assumptions made when the job was first quoted.
A quote is a snapshot, not a production guarantee
The material picture changes as a project moves from quote to order to production. Rubinstein describes a quote as a snapshot of conditions on the day it was prepared. A supplier may have limited reason to investigate every detail deeply until there is a stronger indication that the work will proceed. After an order is placed, customer and supplier have more reason to resolve what is actually expected: which parts matter, when they are needed and how the build should proceed.
That review has to account for current availability, price and backlogs. A component assumed available during quoting may no longer fit the plan by the time the order is active. Some parts may need a closer look than others, and schedule decisions depend on knowing which items are truly blocking. The quote remains useful as an initial reference, but it can’t serve as a live inventory picture throughout the project.
Production is the point where the plan becomes physical. Before then, the team has opportunities to clarify which parts are required and reconcile changes in the design or order. At the production stage, mismatched information can turn into a missing kit, a stopped line or a product built to the wrong revision. Richart’s description of manufacturing as a “binary outcome” captures the constraint: a board either meets the intended requirements or it doesn’t. The floor can’t simply treat an incorrect build as a software issue that will be fixed tomorrow.
The processes involved may run in parallel, but they remain interdependent. Procurement can be working from one part list while program management has learned about a revision. Production may then receive material that is present but no longer correct for the current build. If the change doesn’t reach the people who purchase, receive and allocate parts, the work can proceed on outdated assumptions.
Keeping those connections current is a practical control on production risk. The important record isn’t only whether an order was placed or whether a component arrived. Teams also need to know which revision the component supports, whether it is reserved for the build and whether all involved groups are working from the same requirements. Without that shared picture, a delay may become apparent only when production asks for a part or begins work.
Three questions for build readiness
Richart frames a supplier’s readiness check around three questions: “What do we have?”, “Are we ready to build?” and “What did we build?” Each question addresses a different point in the job, from material status to production readiness and the record of the completed work.
What do we have? This starts with whether material has arrived, but physical presence alone may not settle the question. Receiving can be backlogged, a component may be hard to locate, or stock may have been set aside without a clear record. The team needs a dependable view of what is on hand and whether it belongs to this build.
Are we ready to build? A part can be in the building without being available to production. It may not have been counted, allocated or placed with the rest of the kit. It could be in a box that nobody can find. Readiness means establishing that the necessary material is accounted for and that production can start with the right version of the job.
Richart describes morning meetings involving stakeholders such as sales, customer service, program management and production planning as a way to examine whether work is clear to build. The practical value is in surfacing gaps across roles. A material status that seems settled to procurement may still need to be confirmed by production planning, while a program manager may know about a design change that hasn’t reached the purchasing team.
What did we build? This question matters after the job is on the floor, especially during NPI and pre-production work. Changes may be handled through email without a formal engineering change order (ECO), leaving a customer or supplier to reconstruct exactly which version was built. A manufacturing record that captures the as-built state helps answer questions if a customer later reports a problem with a board.
For Richart, tracking the work doesn’t end when production starts. Teams need to retain enough information to describe the finished build accurately. Capturing those changes supports a useful answer to the customer and gives the manufacturer a clearer account of what happened on the floor. That requires attention to the record as well as to getting the job moving.
Bring the contract manufacturer into design work early
Early contact with a contract manufacturer (CM) can help with both part availability and manufacturability. The CM may have supplier relationships or practical sourcing knowledge that isn’t visible through online availability tools. That input can help a design team understand whether a planned component choice and schedule remain workable as the order takes shape.
The manufacturing review can also catch design choices that would be expensive to revisit later. Richart gives a stackup decision as an example: a designer and fabricator can discuss the proposed board construction while changes are still manageable. If a stackup turns out not to work after the design has advanced, the team may have to return to redesign and lose weeks. Richart describes a customer discussion in which the team raised the issue under time pressure because a failed stackup could send the design back through another four weeks of work.
That example shows why DFM/DFA input belongs early in the schedule. A CM’s experience with building a product can help the design team examine whether its choices suit the intended manufacturing process. The value is not limited to preventing a single difficult board build. Catching a concern before the design is locked can avoid a revision cycle and reduce the chance that a manufacturability issue appears only when production is expected to start.
The same early conversation helps keep the material plan connected to the design plan. If a component or board choice changes, procurement and program management need to know what the change means for the order and the build. The sooner the supplier and customer make that connection, the more time they have to adjust. A design that is finished on paper still needs to be translated into a buildable, supplied and understood job.
Software and manufacturing experience have different roles
MetisLogic brings together Richart’s manufacturing background and Rubinstein’s experience in software engineering and operations. Rubinstein describes himself as a former engineer who had spent his career at software companies including Apple, Netscape and Electronic Arts. His electrical engineering degree gave him a link to the technical side of the manufacturing problem, while his software work shaped how he approached tools for engineers.
Richart’s experience is rooted in circuit board fabrication and quick-turn NPI work. He later joined a contract manufacturer where the initial idea was to improve delivery by making machines go faster. His experience with NPI led him to question whether machine time was the main constraint. For those builds, he concluded, delays often accumulated before the job reached the machines.
That mix of backgrounds informs how the company approaches manufacturing software. A tool may organize information, but it also has to match the way people source parts, manage changes and prepare work for production. Richart says that having worked through delivery problems himself helps the team understand the situations manufacturers describe. For users, the relevant question is whether a tool reflects the handoffs in their actual workflow rather than simply adding another place to enter data.
The first-mile problem is especially visible when teams are managing a changing design, a limited quantity and a short delivery window. Software can help expose what is known about parts and job status, but it still depends on useful information being recorded and changes reaching the people who need them. The workflow has to support decisions across the project, from the first availability check through the final account of what was built.
Where AI may help, and where engineering judgment still matters
Richart sees AI as a useful tool for some product and data work, but he doesn’t expect it to run NPI manufacturing on its own. MetisLogic uses AI in discussions and to process product definitions. Richart also describes the company’s earlier planning work, including a 300-page manifesto written during its first six months, before AI became part of its day-to-day tools.
His view is that AI still falls short on decisions that require an experienced manufacturing engineer to interpret a particular board and process. He points to questions such as how a board differs from another one, what reflow profile will suit it and whether a component arrangement calls for a step-down stencil. These decisions involve applying manufacturing knowledge to the specifics of the job, not just finding patterns in a large volume of text or data.
Richart is more hopeful about AI helping teams find relationships across data that might otherwise be difficult to connect. In his example, analysis might help identify ways to make reflow profiles faster. That would make AI a supporting tool for engineering work: it could help people examine information and generate useful leads while a skilled engineer remains responsible for judging what fits the build.
For manufacturers, the immediate takeaway is to look closely at the time between design completion and production start. Track what has been ordered and received, connect changes to the right people, confirm that material is allocated and keep a record of the build that actually took place. On short NPI and pre-production jobs, those checks can determine whether a ready machine is building on schedule or waiting for the project around it to catch up.