Co-Packaged Optics Testing Shifts Toward Earlier Screening and Failure Isolation
- Laura Peters
- 912 reads
As optical engines join costly ASIC and GPU packages, manufacturers face higher test costs, tougher fault isolation and a need for coordinated production methods.
Testing an optical engine can cost nearly as much as making it, according to surveys cited by ISE Labs fellow Dave Armstrong. As co-packaged optics (CPO) integrates optical components alongside high-value ASICs and GPUs, that cost becomes easier to justify: a small photonics failure can put a much more expensive package at risk. The engineering challenge is to find faults before assembly, then isolate failures in systems where electrical and optical functions share a signal path.
That shift raises practical questions about measurement boundaries, reference light sources, test access and coordination between photonics and semiconductor manufacturing teams. Matt Griffin of Teradyne, Ira Leventhal of Advantest America, Armstrong of ISE Labs, part of ASE Group, and Kazuo Yamaguchi of Keysight Technologies discussed how those issues affect diagnosis and the route to high-volume manufacturing.
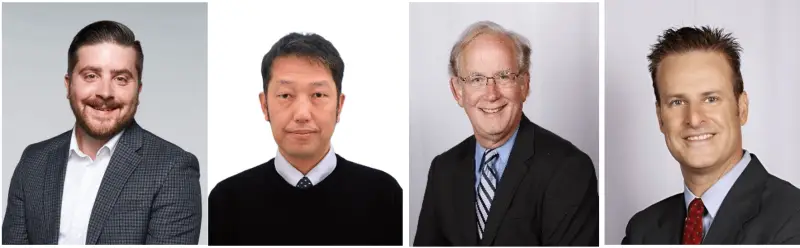
Fig. 1: (L-R): Teradyne’s Griffin; Keysight’s Yamaguchi; ISE Labs’ Armstrong; Advantest’s Leventhal
Define the measurement boundaries
Failure analysis starts by agreeing on the reference plane: the physical, electrical and optical boundary at which a measurement is made. Yamaguchi points to possible reference locations at the die pad, package balls, connectors or fiber interface. Those choices matter because every probe, socket, trace, connector and patch cord between the instrument and the device can affect the measured result.
Teams need to account for those intervening elements, or de-embed their effects, and keep the same boundaries across successive test insertions. If the reference plane changes, a result from one stage may not be comparable with a result from another. To test an optical engine independently, engineers can replace neighboring components with a characterized substitute. A known laser source can stand in for the surrounding optical system, allowing the engine to be evaluated under controlled conditions.
That approach depends on knowing which parts of the setup can be treated as good. Leventhal cautions that the purpose is to test the device under evaluation, not to turn the laser source into another device under test. He compares the source to an electrical device power supply: it is an assumed part of the test setup, and the fault search should focus on the component being tested unless evidence points elsewhere. A laser used in normal operation may not be an automated test instrument, however, so test methods and equipment will need to develop as production needs change.
Test access helps explain a failed link
Monitoring features can make failure diagnosis more direct. Griffin says some designers are adding monitor photodiodes to optical paths so unexpected transmit or receive results can be traced to a location. Loopback testing can also include a tap that routes part of the signal to characterization equipment or allows power monitoring.
This access is useful when a team wants a functional or mission-mode check without running a full characterization sequence. But a loopback pass or failure alone may not reveal why a link misses its bit error rate target or why a program has a functional problem. A tap point gives engineers a way to inspect the signal within the path and narrow the cause. The design decision is therefore about more than passing a test: it determines how much evidence will be available when a system fails.
Integration makes fault isolation harder
Near-packaged optics (NPO) and CPO do not have universally consistent definitions, Griffin notes, and their diagnosis challenges overlap. Both require alignment of multiple optical connectors while electrical power is delivered to the device. One possible distinction is whether an optical engine can be detached from an NPO assembly. Detachability may allow a failed engine to be removed, but reworking and reattaching components later in the process can be difficult. Manufacturers may still prefer to verify that an engine is good before it is integrated.
CPO puts more functions onto a shared package, increasing the need for ways to separate them during diagnosis. Leventhal says design for test can help by exposing information about individual components and making it possible to relate component-level measurements to package failures. That access matters when a system’s symptoms do not point cleanly to one part.
The distinction between two NPO architectures shows why. A retimed NPO has its own digital signal processor (DSP), so the optical engine can be tested for compliance on its own, much like a pluggable module. A linear-drive NPO removes that DSP. Instead, the host ASIC’s SerDes drives the optics through linear drivers and transimpedance amplifiers (TIAs). The electrical and optical sections then act as one signal path, making a failed link difficult to assign to either side. Yamaguchi says the diagnosis challenge is consequently comparable to CPO.
Thermal behavior adds another constraint. Armstrong highlights high power dissipation and the limited distance electrical signals can travel in CPO. NPO may allow greater electrical reach, but that brings its own need to manage the path. In either case, heat from optical components must be considered alongside the electrical design and the package’s operating conditions.
The package changes the test economics
When an optical engine is inexpensive relative to the ASIC or GPU around it, its individual price is an incomplete guide to how much testing makes sense. Leventhal gives the example of a $40,000 or $50,000 GPU or ASIC that could be lost because of a faulty optical engine. In that context, more extensive early testing may be economically reasonable, even if it raises test spending. As production scales and yield information accumulates, manufacturers can refine their test approach.
Yamaguchi sees the same change in the rising value of the device, scrap cost, test complexity and package complexity. That combination makes wafer-level or optical-engine-level screening more attractive before assembly. It shifts some of the emphasis toward identifying weak components early, rather than relying mainly on tests after packaging.
Griffin adds that optical engines support functions that matter to data-center accelerators and network switches, including lower power and disaggregated compute architectures. Their value in the finished system is therefore not captured by considering the engine alone. Manufacturers want to deploy these complex devices efficiently, which keeps pressure on test throughput even as the cost of a missed defect rises.
Scaling needs shared engineering decisions
Leventhal says the industry has already demonstrated that CPO can work, pointing to reliability data Meta presented earlier in the year. The harder task now is turning working systems into high-volume manufacturing. In the near term, he expects manufacturers to use additional screening, burn-in, more test insertions and tighter engineering controls while the broader ecosystem matures. NPO can provide a lower-barrier route to production experience, with lessons that may help CPO scale; that progression still requires work across multiple parts of the supply chain.
Shared standards and multi-source agreements can help align platforms and production expectations, Yamaguchi says, though they do not change the underlying measurement science. Test criteria also need to specify operating conditions such as the optical power to transmit and the bias to apply. Those details give manufacturers a clearer basis for preparing production requirements and defining what a component must deliver.
The equipment choices involve trade-offs too. Griffin describes two groups that often need to work together inside a company: photonics teams, experienced in testing optical devices, and semiconductor test teams, focused on uptime, software and service support, and deploying many test cells. A setup optimized for flexibility, modularity or serviceability may not deliver the same optical performance as another arrangement.
Connector selection makes the consequences concrete. A design may gain flexibility or channel capacity while delivering slightly less optical power at the device under test. That change can affect the device design, so test engineers and photonics designers need to weigh it together with manufacturing teams. Armstrong’s estimate that optical-component test costs already approach manufacturing costs—and may exceed them as complexity grows—reinforces the need to account for test early in the design. The next step is to make component screening, package diagnostics and production equipment choices work as one manufacturing plan.


