WAAM3D Shifts Wire Arc Additive Manufacturing Toward Qualified Aerospace Parts
- Michael Petch
- 468 reads
WAAM3D is pairing wire arc deposition with process knowledge and finishing as aerospace customers seek qualified parts with shorter lead times.
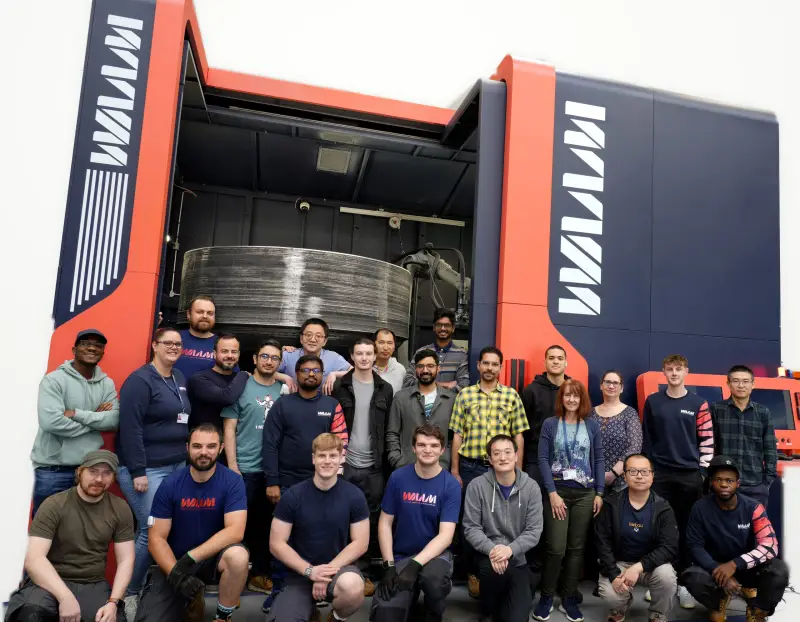
WAAM3D’s commercial opportunity is moving from selling wire arc additive manufacturing equipment toward supplying finished parts. That shift reflects a practical constraint in aerospace: customers need confidence in a component’s integrity and repeatability before they can adopt a new production route. The Milton Keynes company is now fielding more requests for machined, qualified components, as well as interest in its machines and process software.
A nose cone made for the Aircraft Research Association (ARA) in Bedford shows how the process can fit into an existing manufacturing workflow. WAAM3D deposited aluminium onto bar stock to create a near-net-shape blank; ARA then machined the part to tolerance and installed it on a wind tunnel model. The cone measured 350 mm long and 190 mm in diameter. WAAM3D says the approach reduced material use by 74% compared with making the shape entirely from bar stock.
That arrangement worked because ARA had the machining capability to finish the component. Other customers increasingly want a supplier to deliver the completed part and take on the work needed to qualify it. For a buyer seeking an alternative to a long-lead forging, investing in a deposition system is only one part of the decision. Outsourcing production can be more attractive if the supplier can also machine the part and demonstrate that it meets the required standards.
Research expertise built into the process
WAAM3D was incorporated in 2018 to commercialise wire-based additive manufacturing research led by Professor Stewart Williams at Cranfield University. Wire arc additive manufacturing, or WAAM, uses an electric arc to melt metal wire and deposits the material along a programmed path. For manufacturers accustomed to machining titanium forgings and removing large amounts of material, the potential appeal is clear: reduce waste and avoid some of the long waits associated with forging.
Cranfield’s work on titanium deposition included a multi-metre frame developed with BAE Systems for the Eurofighter Typhoon. The team received a 2019 3D Printing Industry Award for the project, but the underlying expertise had accumulated over years of research. Some WAAM3D staff have worked on the process for more than 20 years.
Generating a torch path is only one part of making a reliable component. Engineers also need to select process parameters that suit the material and geometry, and understand how the deposited metal will behave. Zsolt Pinter, WAAM3D’s sales and business development manager, describes the commercial advance as bringing software, hardware and intellectual property together so research knowledge can be used in a customer’s production process.
Cranfield continues early-stage research, while WAAM3D develops the equipment and processes customers can operate. Pinter sees the accumulated knowledge of how to deposit particular materials in particular shapes as the company’s most valuable intellectual property. The goal is to carry that knowledge with the machine rather than leave customers to work out the process from first principles.
Managing heat as geometry changes
WAAM3D serves both research users and manufacturers. Its smaller MiniWAAM is aimed at universities and Catapult centres that want to study materials, test sensors or develop control software. For larger production work, the company offers RoboWAAM Advanced and RoboWAAM Plus. Depending on configuration, the Plus can handle builds up to two metres in each dimension.
WAAM3D advertises deposition rates of up to 15 kg per hour for the Plus and a fivefold increase in process speed. One of its process technologies, patented GMAX, addresses a control problem that becomes more demanding as a part’s geometry changes: managing heat while maintaining material deposition.
GMAX feeds two wires, one energised and one unenergised. According to Pinter, this separates energy input from material input, allowing the operator to vary heat while keeping deposition rate constant. That matters at intersections, where the amount of surrounding metal available to draw heat away changes. The same settings can produce a different bead profile as the torch moves through these features. Adjusting heat while maintaining metal flow can help control both the shape of the build and the fusion between successive deposits.
A robotic welding cell can follow a prepared joint. In WAAM, each new layer is deposited onto a surface created by the previous one, so the process has to account for the actual part as it develops. WAAM3D’s ShapeTech system measures the distance to the deposited surface and maps layer height. A spike in the map gives an engineer a point to inspect after a build. Pinter sees potential for this kind of measurement in future non-destructive testing. He says some automatic correction capabilities are available, while others remain in development.
Qualification sets the pace for aerospace use
WAAM3D’s work with Airbus began more than a decade ago, before the company was formed. Pinter says recent work has focused increasingly on qualification. The material savings possible on a forged titanium component can prompt interest, but aerospace customers need evidence that repeated builds will meet the component’s requirements.
That is why machine throughput alone doesn’t settle the case for production. A deposition rate measured in kilograms per hour says how quickly material can be added; it does not establish whether a completed part has the required quality and integrity. Pinter describes qualification as the largest hurdle to industrial use at scale, particularly in aerospace, where customers need a dependable process before changing how they source a part.
Shorter lead times can still make WAAM compelling. Pinter says a forge might quote more than a year for an order of one or two parts, while WAAM production may reduce the wait to two weeks or five days, depending on the part. He points to replacement components for vessels as an example of the cost of delay: the owner may continue paying for a ship that cannot be used. He gives no comparable delivery estimate for a qualified aerospace component.
Pinter sees aerospace as the sector closest to industrial-scale adoption and identifies obsolete medium-to-large components as another area of demand. He is cautious about predicting when uptake will accelerate, since many of the parts drawing interest in aerospace and nuclear applications are mission critical and can be difficult to qualify. The immediate commercial signal is the change in customer requests: some buyers want to develop processes on their own equipment, while others already know which part they need and want a supplier to deliver it.
Investment and production across two sites
Accuron Technologies, a Singapore-based precision engineering group, became WAAM3D’s first strategic investor and acquired a majority interest in December 2023. Pinter says the backing gave the company time to develop its processes while customers worked through qualification. It also enabled WAAM3D to produce parts in Singapore, closer to customers in the Asia Pacific region.
The company distinguishes that manufacturing role from its engineering base. Singapore is an additional production location, and manufacturing partners supply components for WAAM3D systems. The research team, intellectual property and development decisions remain in Milton Keynes. Pinter describes the core technology as developed in the UK.
A US site lets customers see parts being built
WAAM3D’s first US RoboWAAM installation is at the Commonwealth Center for Advanced Manufacturing (CCAM) in Virginia. In January 2026, the company announced that it had commissioned two systems there: a RoboWAAM equipped with GMAX and an open system using conventional gas metal arc welding. US manufacturers can bring prospective applications to CCAM and see locally how the process performs.
The arrangement also gives WAAM3D contact with the manufacturing problems brought to the centre by its member companies. Seeing a deposited part in person can help a customer assess an application beyond what a presentation can show. For a UK machine builder competing with suppliers able to operate at much larger scale, Pinter’s case rests on process knowledge, intellectual property and engineering experience. Customers can buy that expertise through a RoboWAAM system, or increasingly through a machined component supplied with the process work behind it.
WAAM3D is scheduled to exhibit at Formnext in Frankfurt from 17–20 November 2026, in Hall 11.0, Stand B11. Its next challenge is turning process capability into repeatable, qualified production that customers can specify with confidence.


